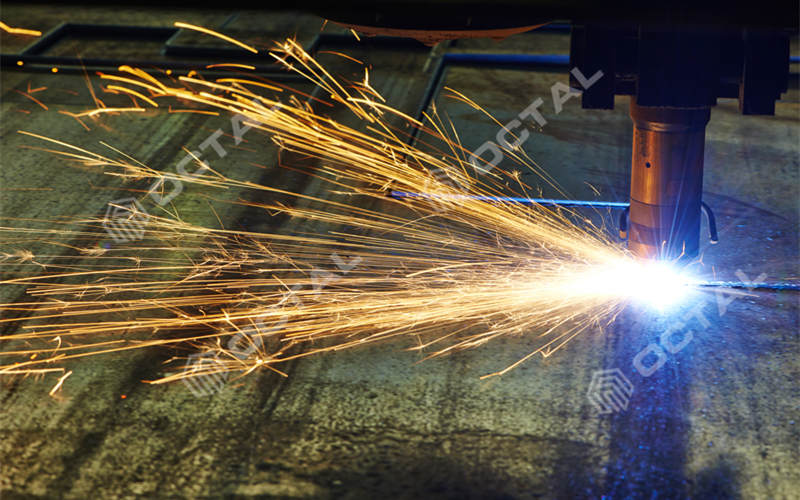
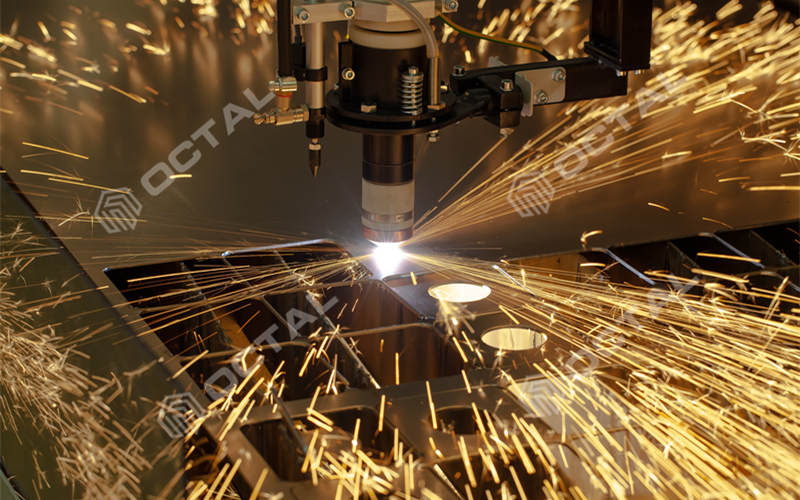
Plasma cutting steel plate uses a high-temperature plasma arc to melt electrically conductive metal, while a high-velocity gas stream removes the molten material and forms the cut. Integrated with CNC control, the torch follows programmed paths to produce straight cuts, custom profiles and angled edges in carbon steel, stainless steel, alloy steel and weathering steel plate for structural and fabricated components.
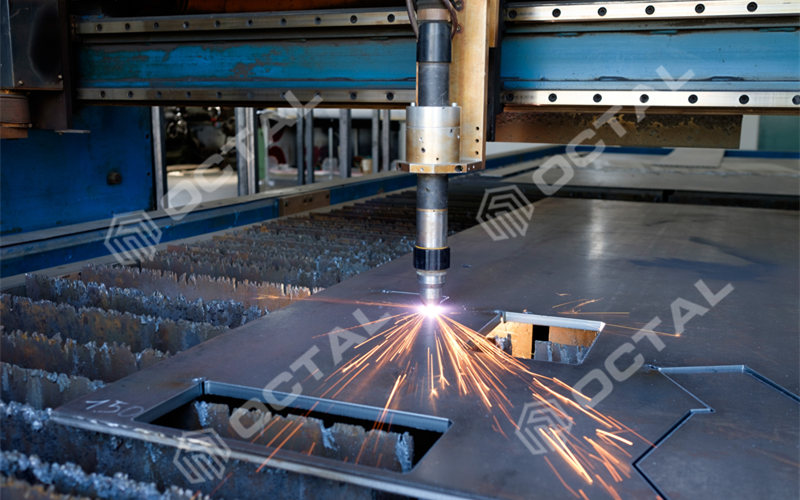
Cutting Material Types
As Plasma cutting is a technique that cuts via electrically conductive materials using an accelerated stream of hot plasma. It could cut many types of material including different steels.
Carbon Steel
Corten Steel
Alloy Steel
Stainless Steel
Aluminum
Brass and Copper
What it is used for?
Plasma cutting is frequently utilized in auto repair and restoration, manufacturing workshops, salvage and scrapping operations, and industrial construction. Because of the very high speed and meticulous cuts coupled with low price, plasma cutting has a wide range of uses from huge industrial CNC operations all the way down to modest hobbyist shops.
Plasma Cutting Thickness
Cutting with plasma is an efficient method of slicing thin as well as thick steel plates and metal materials. Hand-held torches are able to cut steel plates as thick as 38 mm (1.5 in), and more powerful computer-controlled torches are able to slice steel as much as 150 mm (6 in) thick. Given that plasma cutters can generate an extremely hot and very focused “cone” to do the cutting, they can be invaluable for cutting metal sheets with more shapes and profiles in rounded or angled designs.
Octal provide plasma cutting services
We could provide plasma cutting as customized as below materials and size ranges:
Carbon Steel
• ASTM A36/ST37
• ASTM A516
• ASTM A537
• ASTM A572
• ASTM A573
• S275
• S355
• SPCC – Cold rolled steel
• EN8
• Galvanized steel
• Tool steel
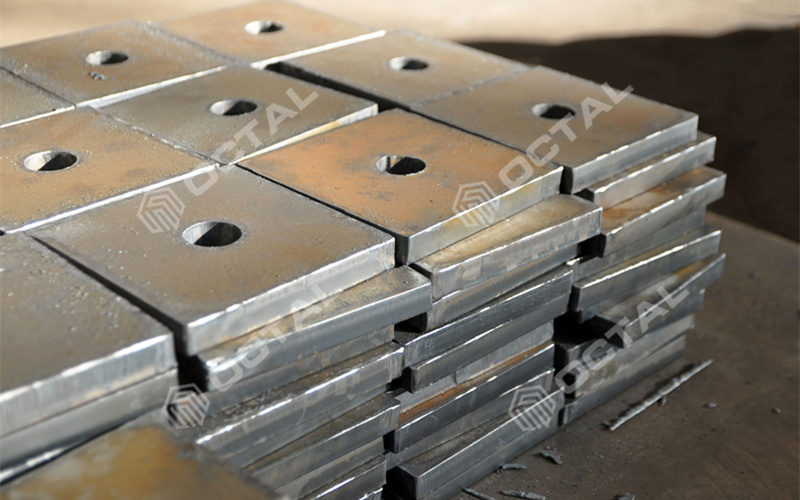
Cutting thickness reach up to 40mm.
Tolerances +/- 1.0 mm/
Stainless Steel
• ASTM 240 304/304L/S30400/S30403
• ASTM A240 316/316L/316Ti/S31600/S31603
• ASTM A240 321/S32100
• 310S/S31008
• 321/S32100
• Duplex steel
• Inconel Alloy 625, 800, 800H, 825
• Hastelloy steel
Cutting thickness reach up to 30mm.
Tolerances +/- 1.0 mm/
Alloy Steel
Chrome alloy ASTM A387
Nickel alloy
Weathering Steel Plate (Corten steel)
• ASTM A242
• ASTM A588 Grade A, B
• Corten A, Corten B
• Weather Steel Plate
How CNC (computer numerical control) integrated in Plasma Cutting
Similar to various other machine equipment, CNC (computer numerical control) technological innovation was used on plasma cutting equipment in the latter part of the 1980s and into the 1990s, providing plasma cutting devices superior versatility to cut various designs “on demand” according to specific details which were programmed into the numerical brain of the machine.
These CNC plasma cutting pieces of equipment was, however, usually confined to cutting designs and components in flat steel sheets, employing just 2 axes of movement (known as X Y cutting)
CNC Plasma Cutting Configurations
CNC Plasma Cutting has 3 primary configurations, which are mostly differentiated by the kinds of materials before working as well as the mobility of the cutting head.
a. 2 Axis Plasma Cutting (2 D)
It is the most popular and traditional kind of CNC Plasma Cutting. Producing level profiles, in which the cut sides have a 90-degree angle to the surface of the material. CNC Plasma Cutting beds, the high powered ones, are set up in this manner, are capable of cutting profiles from metal plate as thick as 150mm all the way up to 30mm thick.
b. 3 Axis Plasma Cutting (3 D)
Just as before, a procedure for creating level profiles from a thin steel plate or sheet metal, but with the advent of an extra rotational axis, the CNC Plasma Cutting machine cutting head is able to tilt even while going through a standard 2-dimensional cutting route. The outcome of this is cut edges at angles besides 90-degrees to the surface of the material, for instances an 30-45 degree angles.
This angle is constant all the way through the material’s thickness. This is usually utilized in conditions where the profile getting cut will be utilized together with a welded fabrication as the edge angle forms a part of the weld groundwork. Once the weld preparation is carried out in the course of the CNC plasma cutting procedure, supplementary functions like milling or machining are often eliminated, thereby minimizing cost. The angular cutting ability of 3D plasma cutting can even be used to produce countersunk holes as well as chamfer edges of profiled holes.
FAQ
Q1: Does one plasma cutting tolerance apply to every steel plate part?
A1: No. CNC plasma cutting tolerance varies with plate thickness, part geometry, torch height, cutting speed and consumable condition. Critical holes, slots or mating features may require secondary drilling or machining when tighter dimensional control is specified.
Q2: Can plasma-cut holes be used directly for bolted connections?
A2: It depends on the required hole diameter, roundness and positional tolerance. High-definition plasma can improve hole quality, but critical bolt holes may still require drilling, reaming or machining when the fabrication drawing specifies tighter acceptance limits.
Q3: Does plasma cutting affect the steel edge before welding?
A3: Plasma cutting creates a localized heat-affected zone and may leave dross or edge angularity depending on the material, thickness and cutting parameters. Weld-preparation edges may therefore require cleaning, grinding or bevel verification before fabrication.
Q4: When is plasma cutting preferred over laser or oxy-fuel cutting?
A4: Plasma is often selected for medium-to-thick conductive steel plate where cutting speed and production cost are more important than laser-level precision. Laser is stronger for fine features and tighter tolerances, while oxy-fuel remains practical for substantially thicker carbon steel plate.
Cutting Steel Standard and Grades
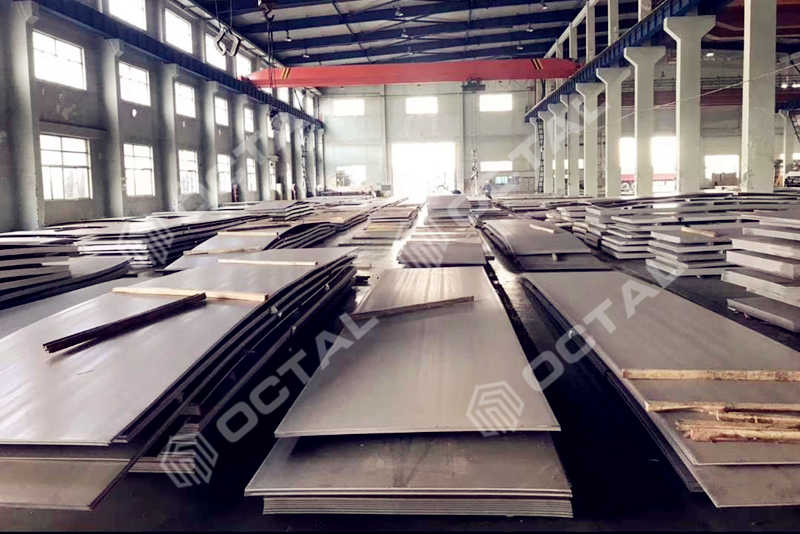
316L Stainless Steel Plate
304 Stainless Steel Plate
ASTM A537 Class 1, 2 Plates
ASTM A572 Grade 50, 60 Steel Plates